Quality inspection has traditionally been a human job, and for good reason. People are remarkably capable at noticing that something is wrong, even when they cannot articulate in advance what wrong would look like. A trained inspector catches defects they have never specifically been taught to find, because human perception is general rather than narrow.
The difficulty is not capability. It is consistency at scale. An inspector examining parts for eight hours does not perform identically in the last hour and the first. Two inspectors apply the same standard slightly differently. And at high line speeds, examining every unit becomes physically impossible, so manufacturers sample and accept that some defects pass.
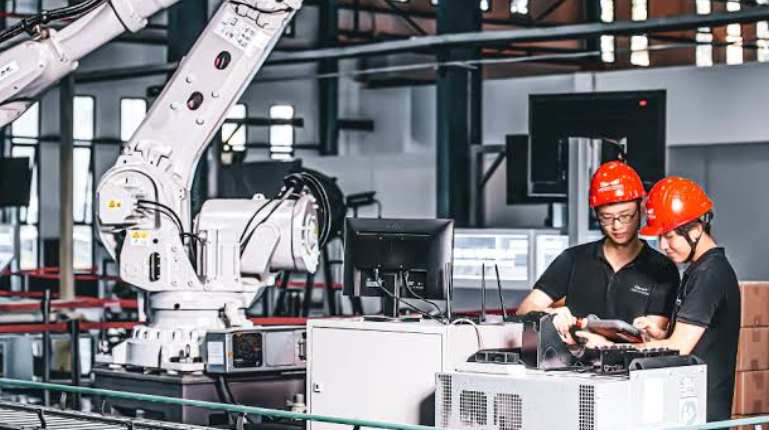
This is the specific gap that automated visual inspection in manufacturing addresses. The technology does not perceive more broadly than a person. It applies a defined standard to every unit, at line speed, without fatigue, and it records what it found.
Where Automation Genuinely Outperforms People
The advantages cluster in specific characteristics rather than being general.
Consistency is the most significant. A system applies the same criteria to the first unit of a shift and the ten-thousandth, which removes a source of variation that is otherwise difficult to control.
Throughput allows one hundred percent inspection where sampling was previously the only option. For high-volume production, moving from sampling to full inspection changes what the quality data means.
Speed exceeds human capability on fast lines, where units pass too quickly for reliable visual assessment.
Precision on dimensional and positional characteristics is far better than visual estimation, since a calibrated system measures rather than judges.
Documentation is automatic. Every inspection generates a record, which supports traceability requirements and makes process analysis possible in a way that manual inspection notes do not.
Repeatability across shifts, lines, and sites means the same standard applies everywhere rather than varying with who is working.
What Humans Still Do Better
Being honest about the limits produces better implementations.
Novel defects are the clearest case. A system trained or programmed to identify specific defect types may not flag something genuinely unusual, whereas a person notices that something looks wrong even when it is a type of wrong they have never seen.
Contextual judgment, meaning assessing whether a marginal defect actually matters for the application, remains a human strength.
Ambiguous cases at the boundary of acceptable frequently need a person to adjudicate, and a well-designed system routes them there rather than forcing a binary decision.
Adapting to change is faster for people. A person told the specification has changed adjusts immediately; a system requires reconfiguration or retraining.
Root cause investigation, meaning working out why defects are occurring rather than whether they are, is analytical work that the inspection data supports rather than replaces.
The productive arrangement in most facilities is automation handling the high-volume repetitive assessment and people handling exceptions, investigation, and continuous improvement.
Applications That Suit the Technology
Certain inspection tasks map well onto automated approaches.
Surface defect detection, meaning scratches, dents, contamination, discoloration, and finish inconsistencies on manufactured surfaces.
Presence and absence verification, confirming that components are fitted, fasteners are installed, and labels are applied.
Dimensional measurement and positional verification, where a calibrated system substantially outperforms visual judgment.
Assembly verification, checking that components are correctly oriented, seated, and connected.
Print and label inspection, covering legibility, placement, and content verification including code reading.
Fill level and seal integrity in packaging applications.
Weld and joint inspection for visible characteristics.
Sorting and grading by visual characteristics, particularly where the criteria are consistent and the volume is high.
The common thread is a defined visual characteristic, assessed repeatedly, at volume.
The Business Case in Practice
The return usually comes from several directions rather than one.
Scrap reduction, since defects caught early stop downstream value being added to a unit that will be rejected anyway.
Rework reduction, which is often a larger cost than scrap and is less visible in reporting.
Warranty and return costs, reduced by fewer defects reaching customers.
Customer relationship value, which is difficult to quantify and is frequently the real driver, since a quality escape with a major customer can affect a contract.
Labour reallocation, where inspectors move to investigation and improvement work rather than repetitive checking.
Process insight, which is the benefit most often underestimated. Full inspection generates data about when and where defects occur, and that data supports process improvements that reduce defect generation rather than merely catching it.
The costs are equipment, integration, configuration, validation, and ongoing support, and they are front-loaded relative to the benefits.
Deciding Where to Start
Implementations succeed more often when they begin narrowly.
Choose an inspection point where defects are currently escaping, or where inspection is a bottleneck, rather than the point that is technically most interesting.
Pick a defect type that is visually distinguishable and reasonably consistent, since an ambiguous defect class produces an ambiguous system.
Establish the current baseline properly: what the defect rate actually is, how it is currently detected, and what escapes cost. Without that, the improvement cannot be measured and the investment cannot be justified.
Involve the inspectors who do the work now, since they know which defects matter, which are ambiguous, and what the conditions on the line actually are.
Plan for the exceptions from the start, meaning what happens when the system flags something uncertain, because a system with no exception path either over-rejects or under-detects.
Then extend to further inspection points once the first one is working, rather than attempting a facility-wide implementation as a single project.